Benefits at a glance
- Extremely quiet
- Consistent operating characteristics
- High abrasion resistance
- Excellent corrosion resistance
- No deposits
Thanks to the use of high-quality materials such as stainless steel and ceramics, liquid ring vacuum pumps are used predominantly in humid and wet processes. This also ensures constant functionality and running characteristics. These vacuum pumps are more reliable than modular pumps and noticeably reduce operating costs.
Application examples
Food / beverage and tobacco industry
- Dairy industry
- central vacuum system
- Filtration systems
- Water degassing in the beverage industry
- Food preservation
- Seawater desalination
- Tobacco humidification
- Sugar production
Packaging machinery industry
- Roll-fed machines
- Filling and sealing machines
- Filling of beer into PET bottles
- Blister machines
Ceramics and brick industry
- Degassing of ceramic bodies
Other applications
- Water degassing
- Groundwater lowering systems
- Drying systems
- Blown air in sewage treatment plants
- Extraction of oil residues
- Steam turbines and steam engines
- Pit extraction
- Lifting and handling
- Yarn steaming in the textile industry
Application examples
Food / beverage and tobacco industry
- Dairy industry
- Central vacuum systems
- Filtration systems
- Water degassing in the beverage industry
- Food preservation
- Seawater desalination
- Tobacco humidification
- Sugar production
Packaging machinery industry
- Roll-fed machines
- Filling and sealing machines
- Filling of beer into PET bottles
- Blister machines
Ceramics and brick industry
- Degassing of ceramic bodies
Other applications
- Water degassing
- Groundwater lowering systems
- Drying systems
- Blown air in sewage treatment plants
- Extraction of oil residues
- Steam turbines and steam engines
- Pit extraction
- Lifting and handling
- Yarn steaming in the textile industry
Benefits at a glance
- extremely quiet
- consistent operating characteristics
- high abrasion resistance
- excellent corrosion resistance
- no deposits
Application examples
Food / beverage and tobacco industry
- Dairy industry
- central vacuum system
- Filtration systems
- Water degassing in the beverage industry
- Food preservation
- Seawater desalination
- Tobacco humidification
- Sugar production
Packaging machinery industry
- Roll-fed machines
- Filling and sealing machines
- Filling of beer into PET bottles
- Blister machines
Ceramics and brick industry
- Degassing of ceramic bodies
Other applications
- Water degassing
- Groundwater lowering systems
- Drying systems
- Blown air in sewage treatment plants
- Extraction of oil residues
- Steam turbines and steam engines
- Pit extraction
- Lifting and handling
- Yarn steaming in the textile industry
Operating principle
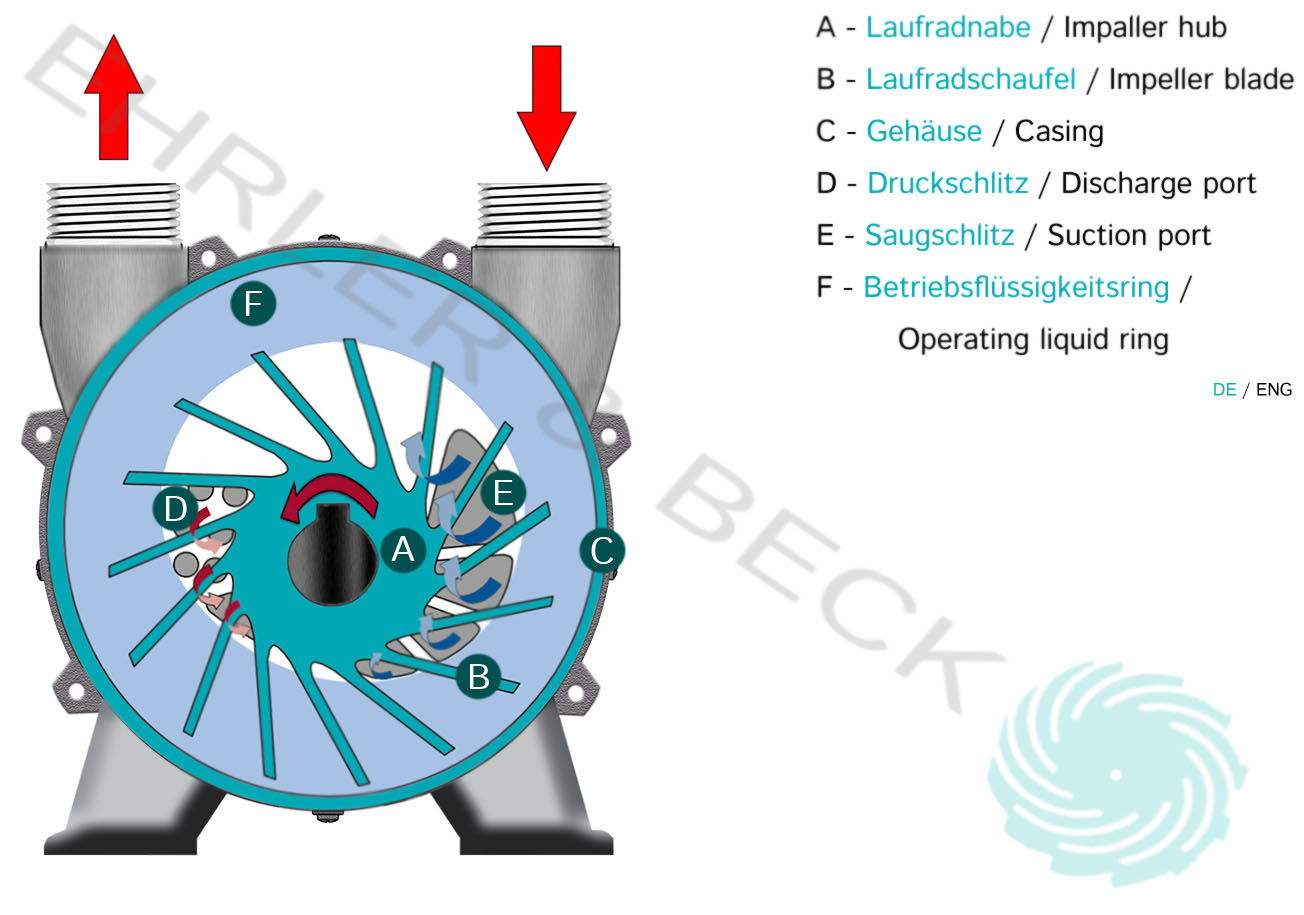
The only moving part inside the liquid ring vacuum pump is the eccentrically mounted impeller (A), which rotates without contact inside the pump housing (C). The operating liquid ring (F) seals the impeller blades (B) from one another. Gas reaches the impeller cells through the suction slot (E). To maintain the stability of the liquid ring with the gas, liquid is continuously drawn into the pumping chamber and discharged again through the discharge slots (D). Owing to the eccentric arrangement of the impeller, gas is compressed within one full revolution, i.e. for the chamber between the blades (B) of the impellers. For stable operation, liquid must be supplied to the pumps continuously. For this reason, the liquid ring vacuum pumps of the L-BL / L-BV series are, as a system solution, equipped as standard with circulation units through which the operating liquid discharged on the pressure side is fed back to the pump. The pump can therefore operate with a considerably reduced liquid supply.
*The description does not take into account each manufacturer’s approach to the technology, but is a general description that attempts to cover the basic operating principle.